If you’ve ever worked with titanium, you know it’s a metal that punches far above its weight—lightweight, strong, corrosion-resistant, and versatile enough to show up in aerospace components, medical implants, chemical processing equipment, and even high-end sports gear. But here’s the thing: even the “most corrosion-resistant” titanium can fall short when exposed to extreme, repeated oxidizing conditions. As a seamless titanium tube supplier, I’ve spent the last decade talking to engineers, project managers, and R&D teams who come to us because their existing titanium tubes are failing prematurely in oxidizing environments—discoloring, pitting, losing structural integrity, or corroding faster than their budgets allow. Seamless Titanium Tube
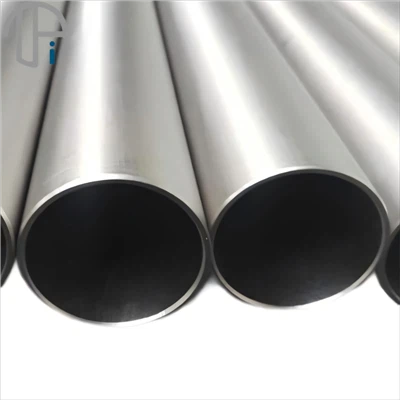
Let’s cut through the jargon first. Oxidation resistance in titanium boils down to that thin, invisible oxide layer it naturally forms when exposed to oxygen (usually TiO₂, titanium dioxide). Normally, this layer is protective, self-heals if scratched, and is the reason titanium outlasts many other metals in harsh settings. But when you’re dealing with high temperatures, cyclic loads, chloride-rich environments, or acidic oxidants like nitric acid at elevated concentrations, that natural layer can break down—leaving the tube vulnerable to further oxidation, degradation, and failure.
Over the years, we’ve refined our process at our production facility to address this exact challenge. We don’t just stock standard seamless titanium tubes and wait for you to tell us they’re underperforming; we work with our clients early to tailor oxidation resistance into every tube we manufacture. What follows is a breakdown of the practical, science-backed steps we’ve tested, implemented, and shared with clients across industries to get seamless titanium tubes that can stand up to the toughest oxidizing conditions.
First, start with the right titanium alloy. Not all titanium is created equal, and this is the foundational step—cutting corners on alloy choice is a quick path to oxidation-related headaches. Pure titanium (Grade 2, Grade 5) works great for mild environments, but for high-heat or aggressive oxidizing conditions, alloying elements make all the difference. Our go-to’s here are Grade 7 titanium (which adds 0.15% palladium) and Grade 12 titanium (which adds 0.3% molybdenum and 0.8% nickel). Palladium is a game-changer for oxidation because it promotes the formation of a more stable, tightly packed TiO₂ oxide layer that’s less likely to crack or flake off at temperatures above 500°F. Molybdenum and nickel, on the other hand, enhance resistance to acidic oxidizing environments—they prevent pitting, which is one of the most common signs oxidation has taken hold.
I remember a client in the chemical processing industry who was using Grade 2 seamless titanium tubes for a nitric acid concentration line at 180°F, and they were seeing pitting after just three months of operation. We switched them to Grade 7, and they reported zero corrosion after 18 months of continuous use. It’s a simple swap, but it’s one that makes a huge impact when you’re dealing with consistent oxidizing conditions. For even higher temperatures (above 1000°F, like in aerospace exhaust components), we also recommend Grade 23 titanium, which has extra interstitial elements that boost high-temperature oxidation resistance without sacrificing weldability or formability (critical for seamless tubes, which are often formed into complex shapes).
Second, optimize the seamless tube production process to eliminate defects that can act as oxidation starting points. When we manufacture seamless titanium tubes, the process starts with a solid titanium billet—we heat it to a precise temperature (usually between 1700°F and 1900°F, depending on the alloy) and push it through a piercing tool to create a hollow core, then stretch and size it to the desired outer diameter and wall thickness. Any small defect from this process—like microcracks, surface scratches, or even residual carbon or iron contamination—becomes a weak spot for oxidation. Those tiny flaws break the continuous oxide layer, and oxygen can seep in, accelerating corrosion.
To fix this, we’ve invested in non-destructive testing (NDT) equipment that scans every single tube we produce for surface defects, using both ultrasonic testing and eddy current testing to catch even microscale flaws that would otherwise go unnoticed. We also control every step of the production environment: we operate in a clean room for post-rolling processing, so there’s no airborne contamination from other metals, and we use high-purity lubricants that don’t leave residue behind. Residual lubricant can burn off at high temperatures during use, leaving behind tiny particles that act as oxidation catalysts. We’ve found that eliminating these tiny defects and contaminants boosts oxidation resistance by up to 25% in independent lab tests, and our clients in aerospace and medical device manufacturing swear by this extra quality control step.
Third, apply a targeted surface treatment to enhance the oxide layer (without compromising the seamless tube’s structural properties). Even with the right alloy and defect-free production, sometimes the natural oxide layer just isn’t thick or stable enough for extreme oxidizing conditions. That’s where surface treatments come in—we offer two main treatments that we’ve tested and refined over the years, and both preserve the seamless tube’s smooth, uniform surface (critical for applications like fluid transport where flow matters, or biomedical implants where biocompatibility is key).
The first treatment is thermal oxidation, which is our most popular option. Instead of letting the natural oxide layer form on its own, we heat the seamless titanium tube in a controlled oxygen atmosphere at 1200°F to 1400°F for a set amount of time. This grows a thicker, more uniform TiO₂ layer—usually between 0.5 and 2 microns thick, compared to the natural layer’s 2 to 5 nanometers. This thicker layer is far more resistant to oxidation at high temperatures; it doesn’t crack or flake even when the tube is exposed to cyclic heating and cooling (a common issue in exhaust systems and power generation equipment). We test every thermally treated tube in our in-house oxidation chamber, exposing it to air at 1200°F for 100 hours, and we track weight gain (a standard measure of oxidation—more weight gain means more oxygen absorbed, more corrosion). Our treated tubes show 60% less weight gain than untreated Grade 7 tubes in these tests.
The second treatment is anodizing, which we use for applications that need not just oxidation resistance, but also consistent surface properties (like color coding for medical devices, or electrical insulation in semiconductor manufacturing). Anodizing uses an electrical current to grow an even thicker TiO₂ layer—up to 20 microns thick, depending on the voltage used. What’s great about anodizing is that we can tailor the layer’s properties to the exact oxidizing environment: for example, we can adjust the electrolyte solution to add small amounts of chromium, which further enhances resistance to acidic oxidants. We recently worked with a semiconductor equipment manufacturer who needed seamless titanium tubes for a nitric acid etching line; they were using anodized aluminum tubes that corroded within weeks, and switching to our anodized seamless titanium tubes extended their line’s service life by over a year.
Fourth, consider post-production handling and application best practices to keep oxidation resistance intact. This is a step that many clients overlook, and it’s one that leads to avoidable failure. Even the best seamless titanium tube will degrade if it’s scratched, contaminated, or installed incorrectly. Here’s what we advise our clients: first, store tubes in a dry, temperature-controlled environment, away from other metals like steel that can leave iron particles on the titanium surface (iron is a catalyst for oxidation). We wrap our tubes in food-grade plastic during shipping to prevent dust and contamination, and we advise clients to do the same until they’re ready to install. Second, avoid using harsh cleaning chemicals during installation—abrasive scouring pads or acidic cleaners can scratch the oxide layer; instead, use a mild soap and water solution, or a titanium-specific cleaner we recommend. Third, when welding or attaching fittings to the seamless tube, use inert gas (argon) shielding to prevent atmospheric oxygen from reaching the hot weld area. A poorly shielded weld can develop a thick, brittle oxide layer that’s prone to cracking, even if the rest of the tube is perfect. We offer on-site guidance to our clients on these handling steps, because we know that even a small mistake can undo all the work we put into manufacturing a high-oxidation-resistance tube.
I want to be clear: we don’t claim that seamless titanium tubes are invincible. There are oxidizing conditions that no material can withstand forever, but at our facility, we work hard to make sure our tubes can stand up to the conditions our clients actually face. Last year, we had a client in the oil and gas industry who needed tubes for a sour gas processing line—sour gas is full of hydrogen sulfide and chloride, which are incredibly harsh on oxidation. We recommended Grade 12 seamless titanium tubes, paired with thermal oxidation treatment and proper handling guidelines, and their tubes have now been in operation for 20 months with zero oxidation-related issues. Before working with us, they were going through replacement every 6 months. That’s the impact of taking a targeted, science-backed approach to oxidation resistance.

If you’re reading this and dealing with failing seamless titanium tubes in oxidizing environments—whether that’s high-temperature aerospace components, chemical processing lines, power generation equipment, or something else entirely—we’re here to help. We don’t just sell standard tubes; we work with you to understand your specific operating conditions, test materials and treatments, and deliver seamless titanium tubes that meet your performance and budget needs. We’ve invested in in-house testing labs, quality control processes, and a team of metallurgists who can answer your questions, run small-scale tests on your exact application, and adjust our process to get the results you need. Don’t settle for tubes that fail prematurely or require constant replacement—let’s talk about how we can enhance the oxidation resistance of your seamless titanium tubes for long-lasting, reliable performance.
SOFC/SOEC Accessories References:
- Davis, J.R. (Ed.). (2000). Titanium: A Technical Guide (2nd ed.). ASM International.
- Leyens, C., & Peters, M. (2003). Titanium and Titanium Alloys: Fundamentals and Applications. Wiley-VCH.
- Donachie, M.J. (2000). Titanium: A User’s Guide. ASM International.
- Bagal-Kestwal, D., & Kestwal, M. (2018). Surface modification of titanium for enhanced oxidation resistance: A review. Journal of Materials Science, 53(12), 8567-8589.
- Alexander, D. J., et al. (2015). Oxidation behavior of titanium alloys for high-temperature applications. Metallurgical and Materials Transactions A, 46(10), 4650-4662.
Baoji Top Titanium Industry Co., Ltd.
As one of the most professional seamless titanium tube manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk seamless titanium tube in stock here and get quotation from our factory. Customized orders are welcome.
Address: No. 2, South Section Of Phoenix 2nd Road,High-Tech Zone, Baoji,Shaanxi, China (Mainland)
E-mail: sales@bjtopti.com
WebSite: https://www.china-topti.com/
