Hey there, Precision Machined Parts
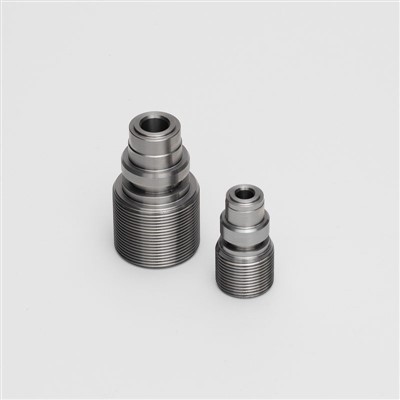
I’m Mia, operations lead at a precision machined parts supplier that’s worked with everyone from aerospace tech startups to medical device manufacturers over the last eight years. Last month, we got a call from a client who’d had a $120,000 batch of custom gear housings rejected because three units cracked during a standard vibration test. The parts had been machined to perfect tolerances—within 0.0002 inches, to be exact—but their shock resistance completely missed the mark.
That call stuck with me, because it’s such a common mistake people make when sourcing precision machined parts: they fixate on dimensional accuracy alone, without stopping to ask, “What will this part actually have to endure when it’s in use?” Shock resistance isn’t just a buzzword for extreme applications. It’s a critical performance spec that can make or break a part’s lifespan, and it’s tied to three specific, non-negotiable requirements that we nail down for every project we take on.
First, there’s material selection tailored to the exact shock profile of the application. A lot of buyers will pick a material because it’s the one they’ve always used, or because it machines easily, without digging into its impact toughness. Let’s break that down. If your part is going into a construction vehicle’s hydraulic valve, it’s going to take sudden, repeated hard impacts from pressure surges. For that, we’d steer toward a alloy steel, like 4140 quenched and tempered to a 28-32 HRC hardness range. Wait, but hardness matters here too—too hard and the part becomes brittle, prone to cracking on impact; too soft and it’ll deform under load. If it’s for a wind turbine’s pitch brake component, which takes occasional, high-energy shock events, we’d go with a higher-alloy steel like 4340, heat treated to a slightly lower hardness (26-30 HRC) to give it a bit of give without sacrificing strength. For medical parts, say a surgical robot’s end effector, we can’t use carbon steel—it’s prone to corrosion. So we’ll pick 17-4 PH stainless steel, precipitation hardened to balance hardness and impact resistance, plus it’s biocompatible. The big takeaway here is that material selection isn’t one-size-fits-all. We always ask clients to share their part’s operating environment—will it see sudden drops, vibration from heavy machinery, thermal shock?—before recommending any material. I’ve seen aluminum 6061 get used for heavy shock applications, and it’s a disaster. That alloy is great for corrosion and easy machining, but its impact toughness is too low for anything beyond minor bumps.
Second, it’s the machining process and surface finish that directly impacts a part’s shock resistance. You can have the perfect material, but if you mill it wrong, you’ll create tiny micro-cracks that become failure points when shock hits. Let’s talk about residual stresses first. When you machine a part, especially with high-speed CNC tools, the friction and cutting force can leave internal stresses in the material. If those stresses are uneven, they’ll pull or push on the part’s structure, making it far weaker to sudden impacts. To fix that, we do a stress relief anneal right after rough machining, before finishing cuts. That step is non-negotiable for us, even if it adds a couple days to the timeline. We’ve had a client test a batch without stress relief, and 15% of them cracked on a simple drop test—after adding the step, zero failures. Then there’s surface finish. A lot of buyers prioritize a mirror-like finish for aesthetics, but for shock resistance, a smoother finish isn’t always better. Wait, hear me out. If you have a part with sharp edges or tool marks left by a CNC mill, those act like stress raisers. A 0.001-inch deep tool mark on a thin wall can double the stress concentration at that point. But if you over-smooth a part, especially with processes like abrasive blasting that remove too much material, you can create a hard, brittle surface layer called a white layer. That white layer is extremely prone to cracking under shock. We balance surface finish: for high-shock parts, we use a controlled vibratory tumble to soften sharp edges without creating a white layer, or if a tighter finish is needed, we use a series of fine end mills to avoid deep tool marks. We also test every batch for surface integrity using eddy current testing—no exceptions. That’s the non-destructive test that checks for micro-cracks or surface defects that the human eye can’t see, and it’s saved our clients (and us) from a lot of costly returns.
Third, it’s design-specific considerations that people often overlook until it’s too late. I know, we’re precision machinists, not design engineers, but we work closely with our clients’ design teams during the quoting stage to tweak parts for better shock resistance. The biggest one is load distribution. If a part has a thin wall or a sharp corner where loads converge, that’s a high-stress spot that will fail first under shock. For example, a client came to us with a custom mounting bracket for a agricultural sprayer—their initial design had a 1/8-inch thick wall at a 90-degree sharp corner, and they were seeing 20% failure rates in field tests. We suggested rounding that corner with a 3/16-inch radius, and increasing the wall thickness to 3/16 inches, which distributed the shock load evenly across the structure. The failure rate dropped to less than 1% after that. Another big design factor is part geometry for mounting. If a part is rigidly mounted at only two points, it flexes unevenly under shock, creating internal stress. If we adjust the mounting to three points (a triangular pattern, which is structurally stable) or add a small relief hole to allow for slight flex, we can improve shock resistance dramatically without changing the part’s original function. We also test for dynamic load, not just static load. A lot of clients do a pull test to check strength, but shock is dynamic—sudden force, not steady force. We use a drop tower test for small parts, or a hydraulic shock tester that delivers controlled, repeatable impact forces to mimic real-world use, so we can validate the part’s performance before it ships. Last year, we did a project for a military ground vehicle’s sensor mount, and the initial design failed a 15g shock test. We adjusted the mounting geometry, modified the material heat treat, and after three iterations, it passed with flying colors. That’s the value of working with a supplier that doesn’t just machine parts from a drawing—we advise on how to make them perform.
Now, I know what some of you are thinking: “I can just source a cheap part and add a shock absorber later.” But that’s a false economy. A $0.50 part that fails because of bad shock resistance will cost you $500 in downtime, replacement parts, and lost productivity. We had a client in the construction industry that tried that: they saved 10% on parts by sourcing from a supplier that skipped stress relief and used a lower-grade steel, and ended up with $200,000 in equipment downtime in six months when parts failed in the field. That’s the kind of cost that makes precise shock resistance worth the investment.
At the end of the day, shock resistance for precision machined parts isn’t a single spec you check off a list. It’s a combination of material selection matched to the load profile, machining processes that eliminate stress and defects, and design tweaks that distribute force evenly. Every part we make goes through a process where we map out exactly what kind of shock it will face, then build to that. If you’re not sure what your part needs, that’s where a good supplier earns their keep.
If you’re working on a project and want to make sure your precision machined parts have the right shock resistance, or you’ve had issues with part failures in the past, reach out to our team. We’d be happy to walk through your requirements, share past project examples, and help you avoid those costly mistakes I talked about earlier. Don’t wait until a field test or a regulatory failure derails your project—let’s get it right from the start.
Shaft Parts References
- ASME B107.300-2010, Standard for Shock and Vibration Testing of Mechanical Components
- ASTM A370-21, Standard Test Methods and Definitions for Mechanical Testing of Steel Products
- Kalpakjian, S., & Schmid, S. R. (2020). Manufacturing Processes for Engineering Materials (7th ed.). Pearson Education.
- Campbell, J. (2012). Manufacturing Technology for Aerospace Structural Materials. Woodhead Publishing.
Taizhou Liuhuan Machinery Co., Ltd.
As one of the most professional precision machined parts manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy customized precision machined parts made in China here from our factory. For quotation, contact us now.
Address: Xinyuan Industrial Zone, Damaiyu Street, Yuhuan City, Zhejiang Province,China
E-mail: tzlhmachining@gmail.com
WebSite: https://www.tzlhmachining.com/
